Field notesSemiconductor manufacturingCase study
Pre-action sprinklers and clean agent systems were too slow for solvent spill fires in a semiconductor plant, and no commercial alternative existed. Archer designed a cylinder-based foam system and proved it through live fire testing.
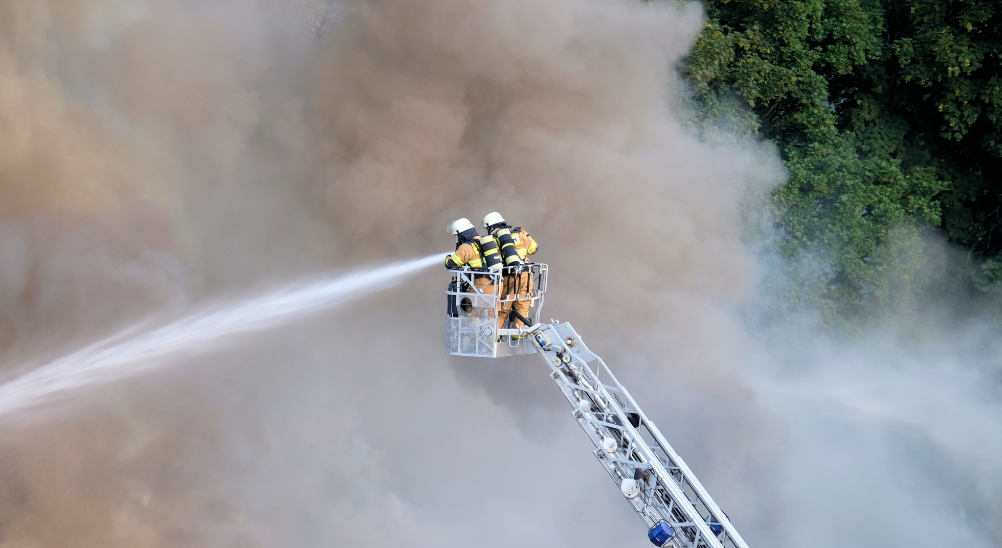
During the first fire tests, the foam discharged on cue but did not extinguish the fire.
The tests were run at a certified Civil Defence testing ground, using ethanol pan fires to exercise the full system logic from flame detection through valve actuation to foam discharge. The aeration and spray pattern from the initial nozzles were not right, and on a solvent fire that is enough to fail.
The system being tested had no commercial equivalent. It had been designed for a semiconductor fabrication plant whose own risk assessment had found a gap. The plant’s statutory pre-action sprinklers and clean agent systems were too slow for the fire most likely to start there.
Why the existing systems fell short
Wafer fabrication relies on volatile solvents. At this plant, some were volatile enough to be ignited by static discharge. A spill can become a pool fire almost immediately, threatening personnel and the process machinery beside it.
Sprinkler and clean agent systems are suited to fires that develop over time. A solvent spill fire develops too quickly for either. The plant needed foam applied within moments of ignition, and evidence that the system would perform before it was installed.
BackgroundThe fire hazards inside a semiconductor fab
- Flammable solvents. Isopropyl alcohol, acetone and other volatile organics used in cleaning and photolithography. Mobile and easy to ignite, so a minor spill is a serious fire. This project
- Pyrophoric materials. Silane and trimethylaluminium, used in chemical vapour deposition (CVD), ignite on contact with air. Trace leaks can burn at once.
- Process equipment. Tools that run hydrogen, toxic gases or flammable vapours at high temperature inside confined enclosures. Wet benches and chemical delivery systems that hold acids and solvents in bulk.
- Static. Automated handling can build enough charge to ignite vapours near the tools.
Adapting a gas suppression design
As no suitable product existed, the team adapted the architecture of a gas suppression system for foam.
Stainless steel cylinders were fabricated, fitted with suppression valves and charged with pre-mixed AR-AFFF, an alcohol-resistant foam suited to polar solvents. Triple IR flame detectors, which register ignition within milliseconds, watched the vats and tools. Nozzles sat directly above the equipment handling the volatile liquids.
For engineersHow the discharge sequence runs
- Detect. Triple IR detectors register the flame within milliseconds.
- Actuate. The release signal energises solenoid valves on the cylinder bank.
- Cascade. Cylinders open in sequence to sustain discharge. Each system has between one and four cylinders, sized to its risk area.
- Discharge. Pre-mixed foam leaves through nozzles over the vats and tools. No proportioner is needed because the foam is already mixed.
The architecture is not tied to one foam concentrate. A change of concentrate, fluorine-free or otherwise, would need its own fire test validation, for the reasons set out below.
Fire testing and nozzle selection
As no comparable system existed, its performance had to be demonstrated by live fire testing. The test ground allowed the plant’s conditions to be reproduced and the full logic, from detector to discharge, to be run on ethanol fires.
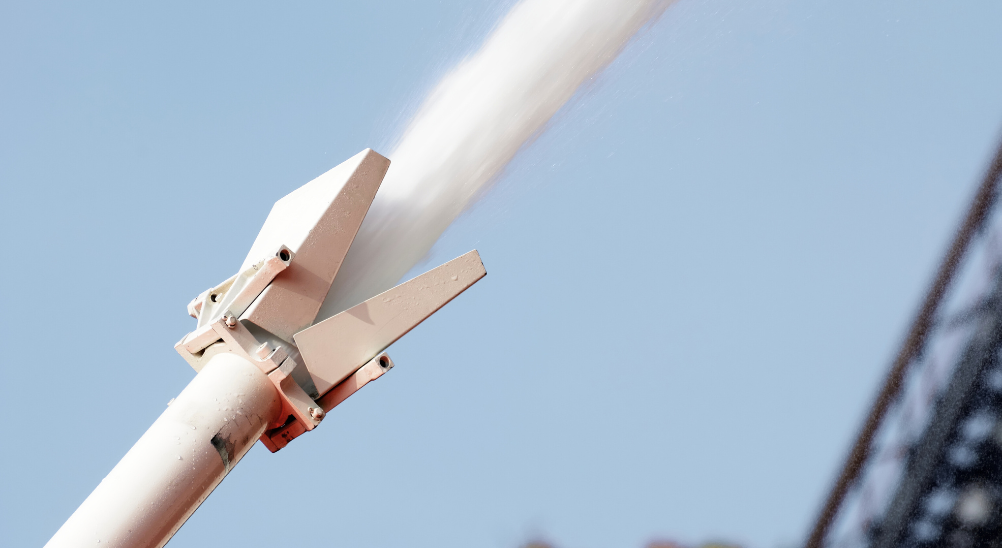
Nozzle selection proved to be the deciding factor. The team tested several types at different pressures, velocities and aspiration characteristics. Each change moved the balance between aeration, which gives the foam blanket its body, and spray pattern, which decides whether the blanket lands on the pool. Small changes in one component produced large changes in the result.
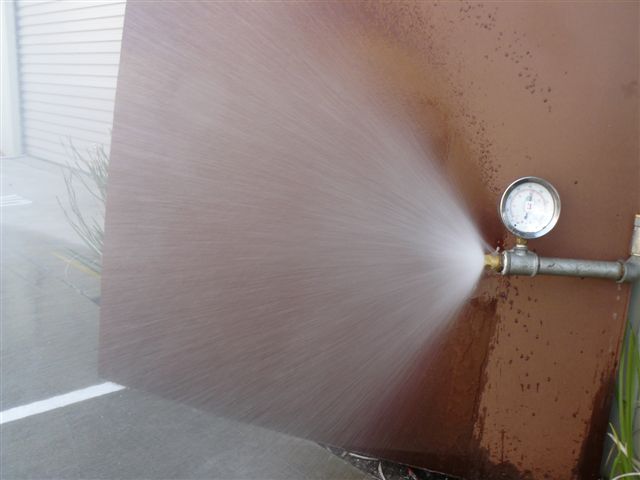
The tests were also run with less foam than the full design basis. A system that passed would carry a two-fold margin once installed.
After several rounds of adjustment, the system achieved rapid, repeatable knockdown. The final demonstrations were witnessed by the authority having jurisdiction.
Every component can carry its own approval and the assembly can still fail.
Lesson from the test programme
Lessons from the test programme
Foam chemistry, flow rate, nozzle design and detection speed all affect each other, and adjusting one changes how the others behave. A foam system therefore has to be tuned and tested as a whole, on representative fires, before its performance can be relied on.
The system went into service with live fire test results that gave both the owner and the AHJ confidence in its performance.